
The tire recycling industry in Australia is rapidly evolving, driven by the need for sustainable waste management solutions and innovative technologies. Tire pyrolysis, a process that converts waste tires into valuable resources such as oil, carbon black, and gas, has gained significant traction in recent years.
This process not only helps reduce the environmental impact of discarded tires but also contributes to a circular economy by turning waste into usable materials. In this article, we will explore the top 10 tire pyrolysis equipment suppliers in Australia, highlighting their offerings and commitment to eco-friendly practices.
These suppliers play a crucial role in promoting sustainable recycling solutions and advancing the tire pyrolysis technology landscape in the region.
What is Tire Pyrolysis Equipment?
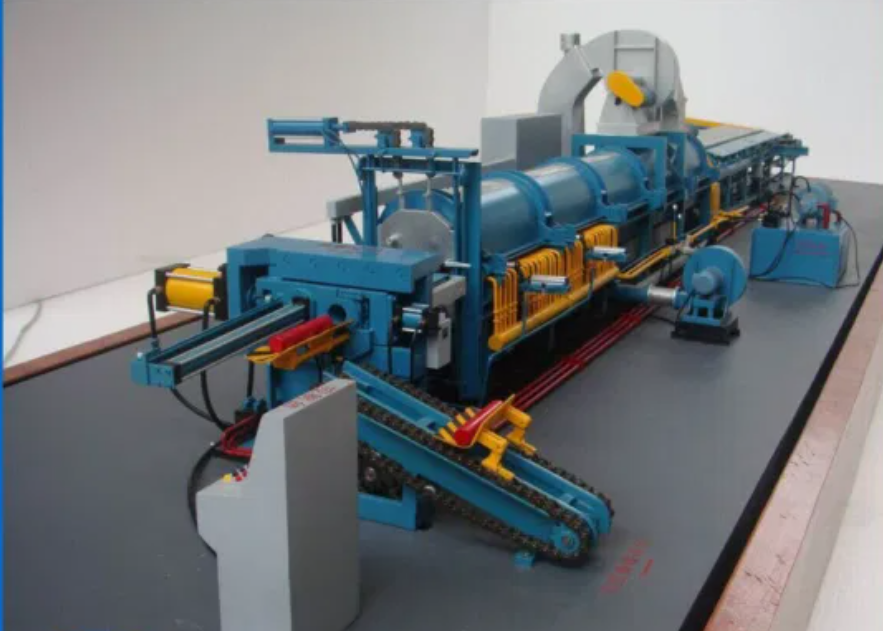
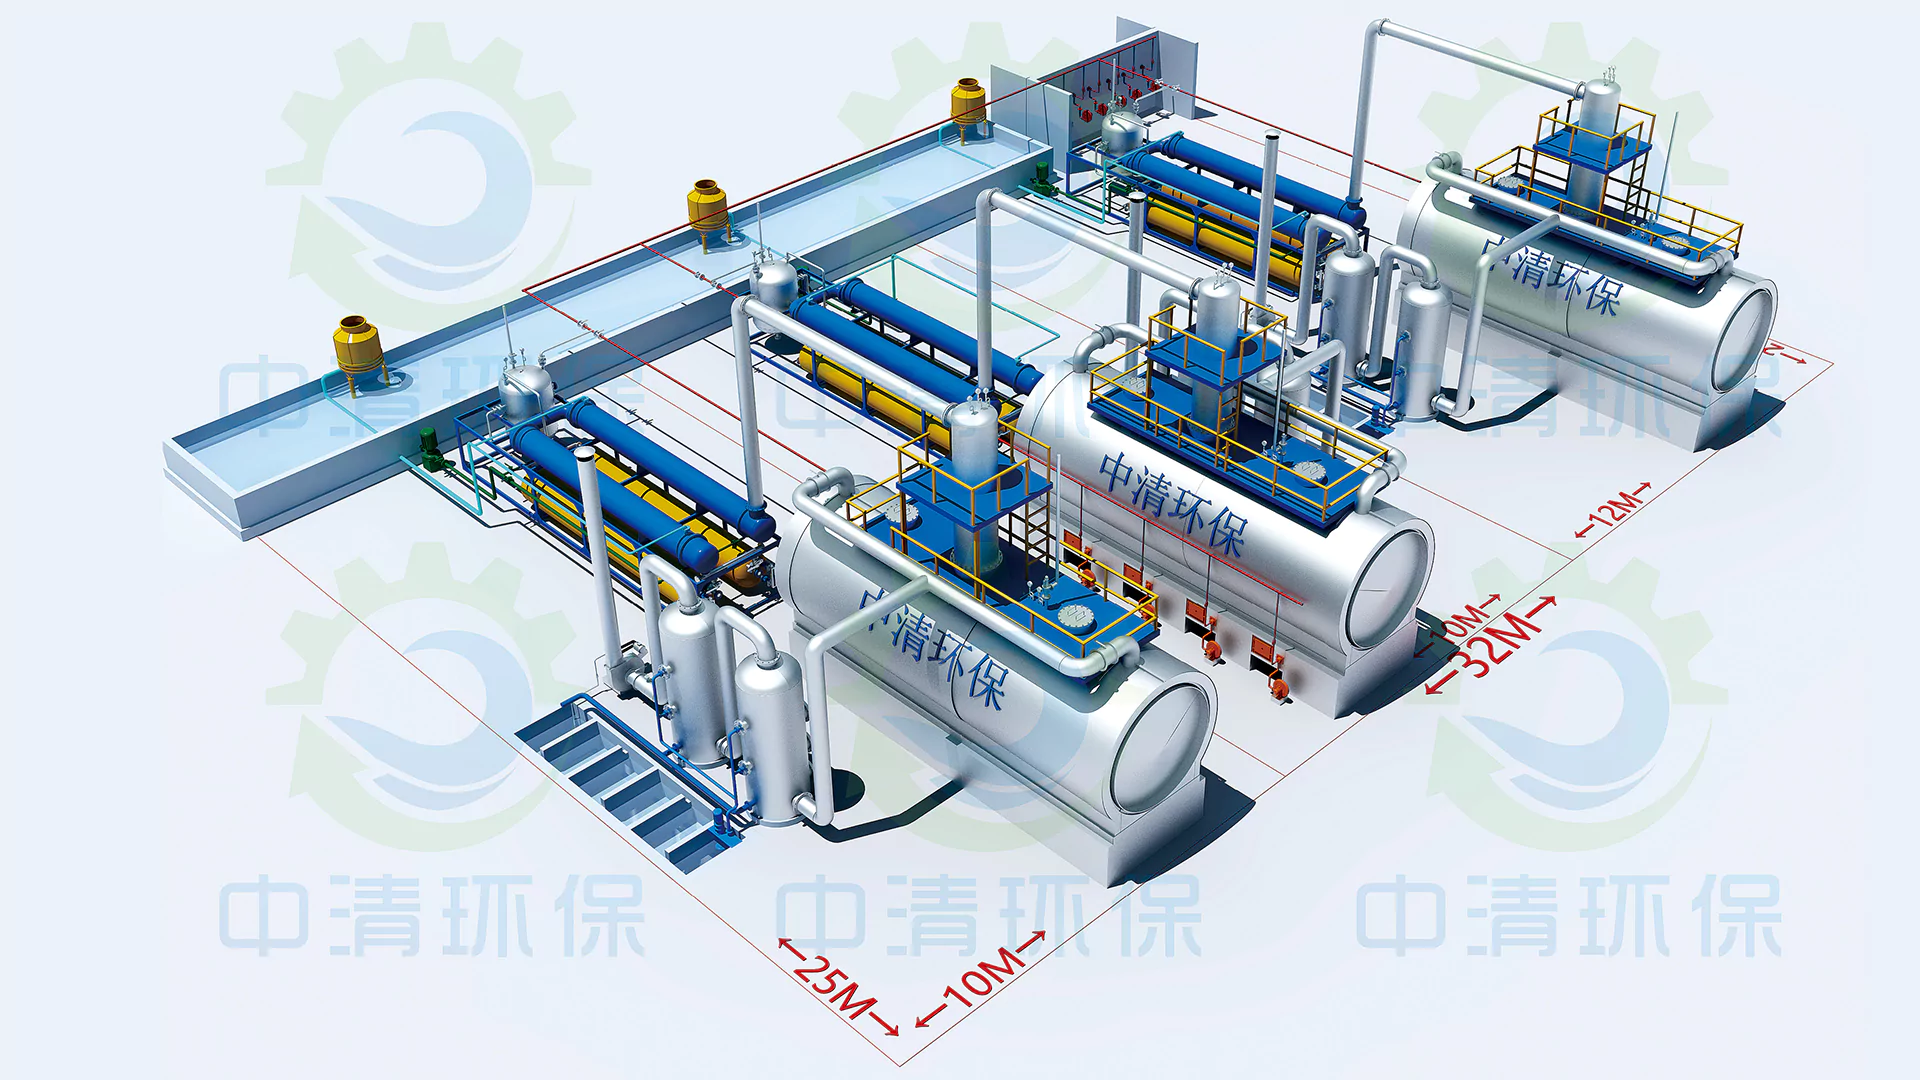
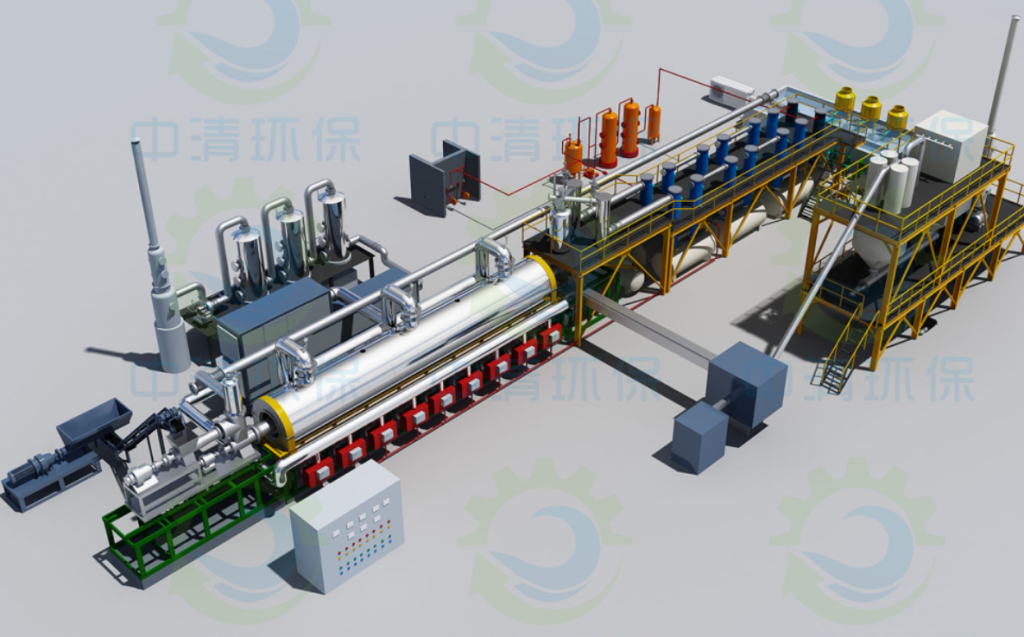
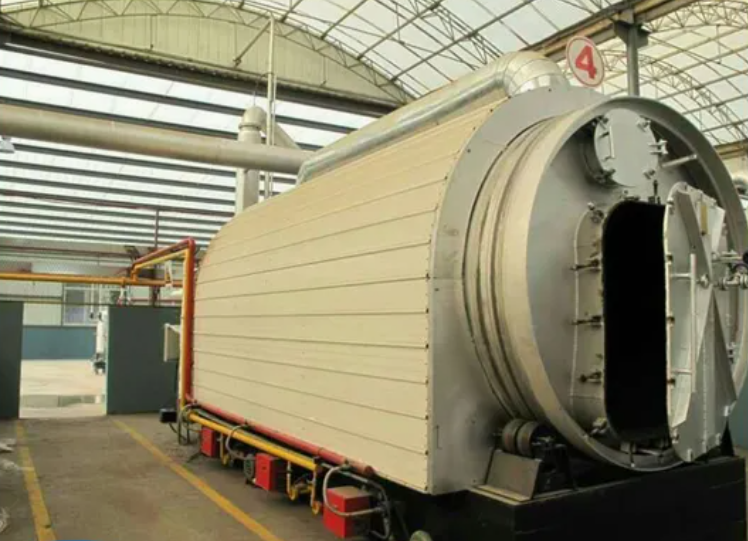
Tire pyrolysis equipment is a specialized system designed to thermally decompose waste tires in an oxygen-free environment. This process, known as pyrolysis, converts tires into valuable byproducts, including oil, carbon black, and gas, through the application of heat.

The concept of pyrolysis as a means to recycle waste materials, including tires, began to gain traction in the late 20th century. It was introduced as a sustainable waste management solution to address the growing environmental concerns associated with tire disposal. The first commercial tire pyrolysis plants started appearing in the early 1990s, primarily in Europe and North America, where regulatory pressures and increased awareness of waste management led to the development of this technology.
Tire pyrolysis equipment has since evolved, with advancements in technology improving efficiency, reducing emissions, and enhancing the quality of the byproducts produced. Today, tire pyrolysis is recognized as an effective method for recycling tires and promoting circular economy practices globally.
What are Benefits of Tire Pyrolysis Equipment?
High-performance tire pyrolysis equipment offers several significant benefits, making it an attractive solution for waste management and recycling. Here are some key advantages:
1. Tire pyrolysis helps significantly reduce the volume of waste tires, which are often difficult to dispose of through traditional methods. By converting them into usable products, the process minimizes the environmental impact associated with tire landfills .
2. The equipment converts waste tires into valuable byproducts, such as oil, carbon black, and steel, which can be reused in various industries. For instance, the oil produced can serve as a fuel source or raw material for other chemical processes, while carbon black is widely used in rubber production .
3. Pyrolysis systems can be designed to be energy-efficient, utilizing the gasses produced during the process to power the equipment itself. This reduces the overall energy consumption and operational costs associated with tire recycling .
4. By reducing landfill waste and recovering valuable materials, tire pyrolysis contributes to a more sustainable waste management approach. It also helps lower greenhouse gas emissions compared to incineration and other disposal methods .
5. The tire recycling industry is growing, creating jobs and business opportunities in manufacturing, waste management, and environmental services. The production of high-quality byproducts can also lead to new revenue streams for businesses involved in tire recycling .
List of Top 10 Tire Pyrolysis Equipment Suppliers:
Klean Industries
Klean Industries is a prominent supplier of high-quality tire pyrolysis equipment, recognized for its innovative and eco-friendly solutions in waste tire recycling. The company specializes in converting end-of-life tires into valuable resources such as oil, carbon black, and steel. Klean Industries focuses on providing high-quality pyrolysis equipment designed for efficiency and sustainability, helping clients minimize waste while maximizing resource recovery.
Their commitment to environmental responsibility has positioned them as a leader in the tire pyrolysis market, offering comprehensive services and support to customers worldwide.
Heavy Industry
Heavy Industry is a premium tire pyrolysis equipment supplier dedicated to creating value for customers while contributing to global environmental protection efforts. The company emphasizes the importance of technological innovation and collaboration with scientific research institutions. By staying attuned to market development needs and advancements in technology, SHANGQIU aims to enhance the safety, health, and environmental protection levels of its products and services.
With a strong team of experienced professionals and experts from the Academy of Environmental Sciences and the Institute of Environmental Protection, SHANGQIU is committed to promoting recycling of waste resources.
Eurotrade Australia
Eurotrade Australia is a supplier of tire pyrolysis equipment for sale that focuses on providing advanced recycling solutions for used tires. The company offers a range of equipment designed to efficiently convert waste tires into valuable products.
Eurotrade emphasizes the importance of sustainable practices and is committed to promoting eco-friendly solutions within the Australian market. With a focus on quality and customer service, Eurotrade Australia aims to support businesses in their efforts to implement effective tire recycling processes.
Beston Group
Beston Group is a leading manufacturer of tire pyrolysis equipment, offering advanced technology for recycling waste tires into useful products. Their systems are designed to maximize efficiency and minimize environmental impact. Beston’s pyrolysis equipment converts tires into oil, carbon black, and steel wire, providing a sustainable solution for waste management.
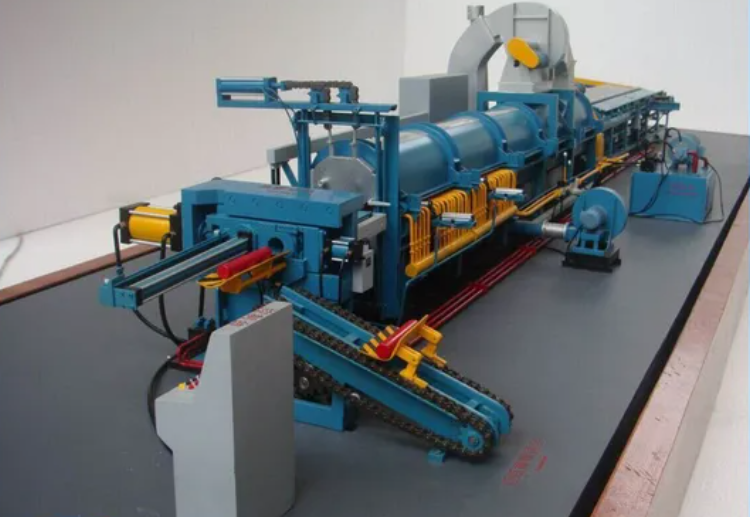
The company emphasizes innovation and continuous improvement, ensuring that their equipment meets the highest industry standards. With a strong presence in global markets, Beston Group is committed to promoting eco-friendly practices and supporting clients in achieving their recycling goals.
Wastetireoil
Wastetireoil specializes in tire pyrolysis technology, focusing on converting waste tires into valuable oil products. Their equipment is designed for high efficiency, allowing for effective processing of used tires while minimizing emissions and waste. The company is dedicated to providing comprehensive solutions for tire recycling, offering equipment that is both reliable and cost-effective.
Wastetireoil’s commitment to sustainability and environmental responsibility positions it as a key player in the tire pyrolysis industry, helping clients transform waste into valuable resources.
Green Distillation Technology
Green Distillation Technology is renowned for its innovative tire pyrolysis solutions aimed at recycling waste tires. Their patented technology effectively converts used tires into high-quality oil and carbon black, contributing to sustainable practices in waste management. The company focuses on reducing environmental impact while providing economically viable solutions for tire recycling.
Green Distillation Technology’s systems are designed to be efficient and environmentally friendly, making them a preferred choice for businesses looking to implement tire pyrolysis processes. Their commitment to advancing recycling technology aligns with global sustainability goals.
Enviro System
Enviro System is a prominent supplier of high-end tire pyrolysis equipment, focused on delivering sustainable solutions for waste tire recycling. Their technology is designed to efficiently convert used tires into valuable products, such as oil and carbon black, while minimizing environmental impacts. Enviro System emphasizes the importance of innovative designs and efficient processes, allowing clients to achieve effective waste management solutions.
The company is dedicated to enhancing recycling capabilities, contributing to a cleaner environment, and aligning with global sustainability initiatives.
Pyrotech Energy
Pyrotech Energy specializes in tire pyrolysis technology, offering state-of-the-art equipment that transforms waste tires into high-quality fuel and other byproducts. Their systems are engineered for maximum efficiency, safety, and environmental protection. Pyrotech Energy’s commitment to research and development allows them to stay at the forefront of tire recycling technology, providing clients with reliable and effective solutions.
By focusing on sustainable practices, Pyrotech Energy helps businesses contribute to the circular economy and reduce their carbon footprint.
Tire Stewardship Australia
Tire Stewardship Australia (TSA) is an organization dedicated to promoting sustainable tire recycling practices across the country. While not a direct supplier of tire pyrolysis equipment, TSA plays a crucial role in the industry by supporting initiatives that encourage the responsible disposal and recycling of used tires. They advocate for the adoption of innovative technologies, including pyrolysis, to manage waste tires effectively.
By collaborating with various stakeholders, including manufacturers, recyclers, and government bodies, Tire Stewardship Australia aims to create a more sustainable tire recycling landscape in Australia.
HUAYIN
HUAYIN is a well-established supplier of tire pyrolysis equipment, recognized for its commitment to innovation and sustainability in waste tire recycling. The company offers a range of advanced pyrolysis systems designed to efficiently convert used tires into valuable resources, such as oil, carbon black, and gas. HUAYIN focuses on delivering high-quality, reliable equipment that meets the demands of the global market while ensuring minimal environmental impact.
Their experienced team is dedicated to providing comprehensive support and solutions tailored to the specific needs of their clients, making them a key player in the tire pyrolysis industry.
Conclusion
In conclusion, the tire pyrolysis equipment market in Australia is supported by a variety of reputable suppliers, each offering unique solutions to meet the growing demand for sustainable waste tire management. From Klean Industries to HUAYIN, these suppliers provide advanced technology to convert waste tires into valuable resources, contributing to environmental sustainability and resource recovery.
Among these distinguished suppliers, Heavy Industry stands out as a leader in the industry, renowned for its commitment to innovation and quality. Their comprehensive approach to enhancing fire safety, coupled with a strong emphasis on technological advancements and customer satisfaction, positions them as an unmatched player in the tire pyrolysis sector.
As businesses seek effective solutions for tire recycling, partnering with SHANGQIU will undoubtedly provide the best outcomes in efficiency, sustainability, and overall performance.